
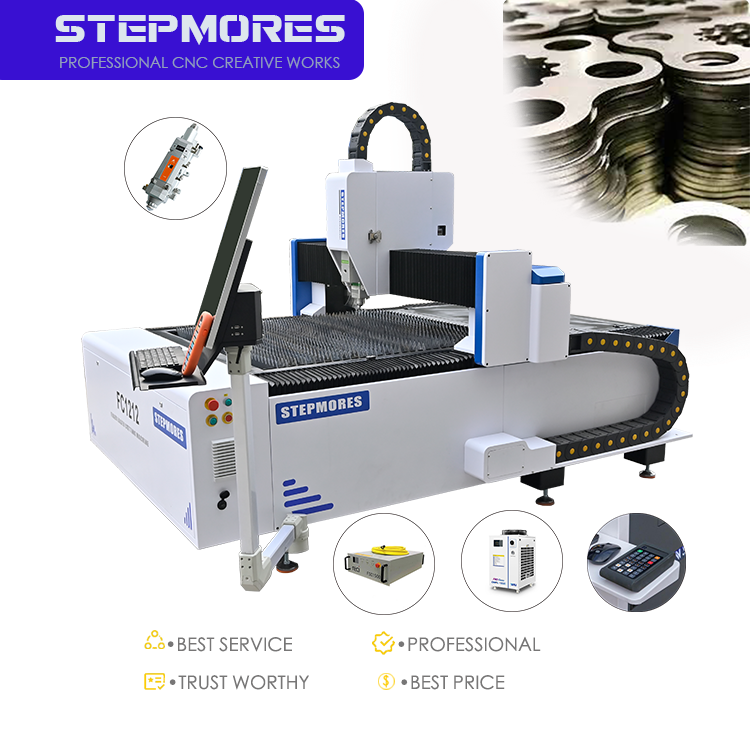
Stainless Steel: High-Precision Processing for Industrial Applications
Why 304 and 316 stainless steel dominate CNC fiber laser cutting machine workflows
Austenitic stainless steels 304 and 316 are the workhorses of modern laser fabrication, processing cleanly in a CNC fiber laser cutting machine with minimal post-cut treatment. Their dominance stems from metallurgical stability and corrosion resistance: the low carbon content of 304 suppresses carbide precipitation during thermal cycling, while the molybdenum addition in 316 further enhances resistance to pitting and intergranular corrosion—critical in chemical, marine, food, and medical applications. Fiber lasers routinely achieve dimensional tolerances of ±0.002–0.005 inches (±0.05–0.13 mm) on these grades, with kerf widths under 0.15 mm and edge roughness (Ra) below 1.6 μm on thin sheets—often eliminating secondary finishing. The fine focal spot (<50 μm), combined with flexible assist gas options—nitrogen for oxide-free edges, argon for weld-critical parts, and compressed air for cost-sensitive runs—enables precise control over edge quality, speed, and heat input. As a result, 304 and 316 account for over 70% of industrial stainless steel laser cutting, valued for predictable heat-affected zone (HAZ) behavior and high repeatability in volume production.
Optimal thickness range (0.5–25 mm), power settings, and kerf quality benchmarks
Fiber laser cutting delivers optimal quality on stainless steel between 0.5 mm and 25 mm thickness, with power and assist gas selection scaling deliberately across this range. For sheet up to 2 mm, a 1.5 kW system cuts at 18–25 m/min using nitrogen at 12–15 bar, yielding kerfs as narrow as 0.10 mm and edge perpendicularity within 0.05 mm. In the 3–10 mm range, 3–4 kW lasers operate at 1.5–5 m/min with kerfs of 0.15–0.25 mm—suitable for “as-cut” architectural and enclosures. At 12–20 mm, 6–8 kW systems typically use oxygen assist to maintain viable speeds, though this introduces a thin oxide layer often addressed with light bead blasting. For 25 mm plate, 10–12 kW lasers cut steadily at ~0.6 m/min; edge taper rises to 1–2° and HAZ extends to 0.3–0.5 mm. Industry data confirm that, with optimized focal position and gas flow, a 6 kW fiber laser can hold kerf width deviation under 0.03 mm across a full 4×8-foot sheet of 304 stainless up to 10 mm—making it the preferred platform for high-mix, low-volume precision fabrication.
Carbon Steel: Balancing Speed, Edge Quality, and Assist Gas Strategy
Selecting the right assist gas and process parameters is critical when using a CNC fiber laser cutting machine on carbon steel, as the balance between cutting speed and edge quality directly impacts downstream operations.
Oxygen vs. nitrogen assist gas: trade-offs in cut speed, oxidation, and post-processing needs
Oxygen remains the standard assist gas for carbon steel due to its exothermic reaction with iron, effectively doubling thermal input and boosting cutting speed by up to 30% compared to inert gases. Typical operating pressures range from 0.8–1.2 bar. However, this reaction forms a thin, hard oxide layer on the cut edge—requiring grinding, blasting, or acid cleaning before painting or welding. Nitrogen, delivered at higher pressures (18–25 bar), produces an oxide-free, weld-ready surface but operates 20–30% slower and incurs significantly higher gas costs per meter. Fabricators prioritizing throughput—such as those producing structural frames—commonly choose oxygen; those targeting visible assemblies, tight-tolerance weldments, or powder-coated finishes select nitrogen. The decision ultimately reflects the acceptable post-processing budget and required surface finish class.
Reliable processing limits for Q235 and A36 up to 20 mm with spatter and dross mitigation
Q235 and A36 carbon steels are reliably processed up to 20 mm using oxygen assist on fiber lasers rated 6 kW and above. At 12 mm, stable cutting occurs at 0.9–1.1 m/min; at 20 mm, speed drops to 0.5–0.7 m/min. Dross and spatter are primarily mitigated through three controllable parameters: focus position, nozzle standoff, and gas purity. Positioning the focal point 0.5–1.0 mm below the material surface ensures full melt ejection and minimizes bottom dross. Maintaining a consistent nozzle distance of 1.0–1.5 mm and using oxygen ≥99.5% purity prevents turbulent flow and top-side spatter. Pre-inspection for rust, mill scale, and flatness is equally essential—surface irregularities deflect the beam and cause striations. With these controls in place, Ra values of 12.5 µm or better are consistently achieved without hand finishing.
Non-Ferrous Metals: Overcoming Reflectivity in Aluminum, Brass, and Copper
Material-specific challenges: reflectivity, thermal conductivity, and surface oxide management
Aluminum, brass, and copper present distinct challenges in fiber laser cutting due to high optical reflectivity, rapid thermal dissipation, and tenacious surface oxides. At the 1 µm wavelength of fiber lasers, aluminum reflects over 90% of incident energy—copper even more—posing a serious risk of back-reflection damage to optics without protective hardware. Their high thermal conductivity—copper’s ~400 W/m·K, aluminum’s ~235 W/m·K—pulls heat away from the kerf faster than ferrous metals, demanding tighter focus, higher peak power, and precise pulse control. Additionally, native oxides on aluminum (Al₂O₃) and copper (CuO/Cu₂O) melt at temperatures far exceeding their base metals, creating inconsistent melting and poor edge quality if not managed. Effective strategies include surface cleaning, nitrogen assist to inhibit re-oxidation, and anti-reflective hardware.
Proven techniques for safe, high-quality cutting of 5052/6061 aluminum and C110 copper
Safe, high-quality cutting of 5052 and 6061 aluminum requires integrated safeguards: back-reflection absorption systems protect optics, while nitrogen assist gas ensures clean, dross-free edges. Process tuning includes elevated pulse frequency and focal positioning just below the surface to concentrate energy and minimize HAZ. An optional black absorptive coating further improves coupling efficiency on highly reflective sheets. Copper C110 demands even stricter protocols—dedicated reflection absorbers, reduced feed rates, and rigorous optics maintenance. Nitrogen assist is non-negotiable: it enables effective melt ejection and prevents oxidation, delivering bright, precise edges. On 1 mm C110, speeds of 1.2–1.5 m/min are achievable with a 1 kW laser; thicker sections require proportionally higher power and calibrated gas dynamics.
Material Compatibility Limits: Metals Requiring Caution or Alternative Methods
While CNC fiber laser cutting offers broad versatility, certain metals pose unacceptable risks without mitigation—or require alternative methods entirely. Key limitations arise from extreme reflectivity, excessive thermal conductivity, or hazardous fume generation.
Uncoated silver, polished high-purity aluminum, and mirror-finish brass alloys reflect so much incident energy that back-reflection can damage lenses, windows, and sensors—potentially causing costly downtime. Even when catastrophic failure is avoided, inconsistent energy coupling leads to incomplete or erratic cuts.
Coated or layered materials also warrant caution. Galvanized steel releases zinc oxide fumes that impair sensor function and pose respiratory hazards—necessitating robust, certified fume extraction. Similarly, manganese-rich alloys or lead-containing metals generate toxic vapors during vaporization, requiring specialized ventilation and compliance with OSHA and local occupational health standards. High-carbon steels (e.g., 1095 or tool steels) cut mechanically but develop a hardened, brittle HAZ prone to micro-cracking—compromising formability and weld integrity.
For all such materials, a formal compatibility test—evaluating cut quality, fume composition, optical safety, and post-process behavior—is essential before production ramp-up. When risks cannot be sufficiently mitigated, plasma, waterjet, or mechanical methods remain safer, more reliable alternatives.
FAQ
What makes stainless steel grades 304 and 316 ideal for CNC fiber laser cutting? - Their metallurgical stability, corrosion resistance, and predictable heat-affected zone behavior make them suitable for high-precision cutting with minimal post-processing.
How does assist gas selection affect fiber laser cutting? - Assist gas types (nitrogen, oxygen) impact edge quality, oxidation levels, and operational costs, tailored to the specific material's cutting requirements.
What challenges arise when cutting non-ferrous metals like aluminum or copper? - High reflectivity, thermal conductivity, and tenacious oxide layers complicate the cutting process, requiring specialized hardware and cutting strategies.
Can all metals be cut with CNC fiber laser machines? - While versatile, CNC fiber lasers cannot reliably cut metals with extreme reflectivity or hazardous fume emissions. Alternative methods may be required.